

The short answer is this: choose PETG when the selling point of the palette is transparency, chemical resistance and a glass-like premium feel, and choose ABS when the selling point is structural rigidity, crisp closure feel, electroplated or painted surfaces and complex geometry. Most successful palette programs actually combine both — an ABS shell that carries the structure and decoration, with a PETG window, tray or lid panel where clarity is required. Before placing a bulk order, a professional buyer should verify four things in writing: the exact resin grade and whether it is virgin material, the certification package covering the destination market (FDA 21 CFR food-contact style documentation, REACH SVHC screening, ISO 22716 GMP at the factory), the decoration and assembly test evidence (drop, hinge cycling, cross-hatch adhesion, pan retention), and the tolerances that govern pan fit, mirror seating and magnetic closure force.
This guide is written for importers, private-label beauty brands, promotional buyers and distributors sourcing eyeshadow palettes and compact cases in volume. It explains what each packaging polymer actually is, how the two dominant engineering plastics for palettes — PETG and ABS — behave in production and in the consumer's hand, which failure modes generate the most complaints and returns, how to verify quality claims with documents and simple bench tests, and how to structure an RFQ so that quotations from different factories are genuinely comparable. It contains only general industry knowledge and does not recommend any specific manufacturer.

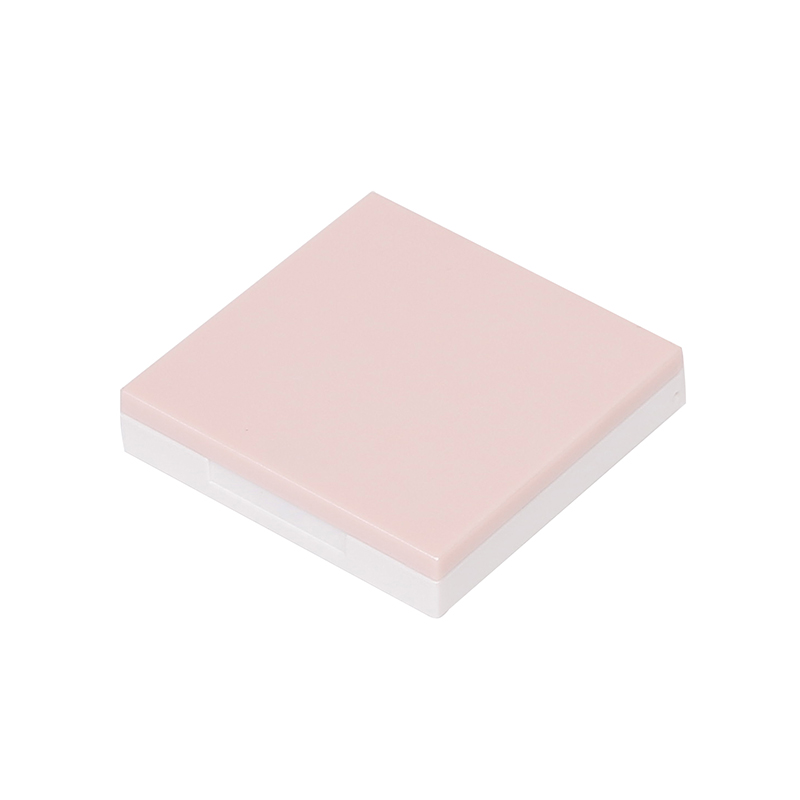
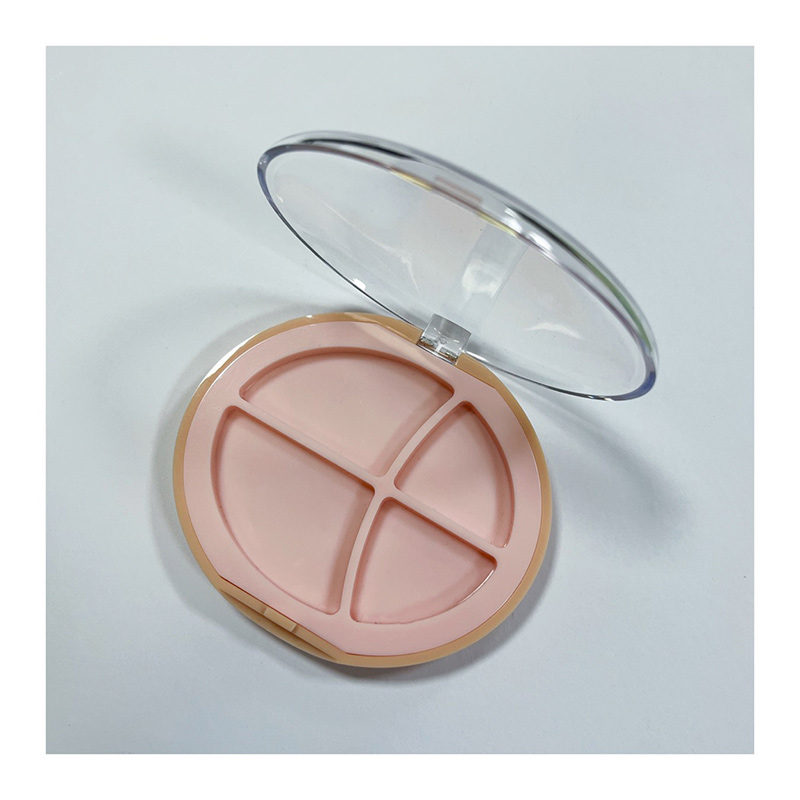
In B2B language, an eyeshadow palette is not one product but an assembly system. It consists of an outer case (the shell, typically injection molded), an inner tray or pan platform (which may be part of the shell or a separate insert), individual pans or wells (empty aluminum or plastic pans that the brand fills with powder or cream), a mirror (glass with a protective backing, seated in a recess or glued to the inner lid), a closure system (snap-fit, magnetic clasp, Sliding cover or hinged flip-top), and decoration layers (paint, electroplating, rubber-touch coating, hot stamping, silk screening or IMD films). Each of those elements has its own material requirements, and the "palette material" question is really a question about five or six material decisions made together.
Buyers who treat the palette as a single line item ("plastic palette, pink, 12 colors") lose control of the two variables that cause most quality complaints: the resin of the structural shell and the interaction between the shell and the decoration system. A shell resin that is perfectly adequate for a plain matte finish can fail badly once it must accept electroplating, or hold a glass mirror against drop loads, or survive repeated flexing at a living hinge. This is why serious factories ask for the full specification — pan count, pan size, closure type, decoration plan, target drop height — before quoting, and why buyers should be suspicious of a quote that arrives without any clarifying questions.
It also matters which market the palette ships to. A palette for a promotional giveaway in a dry climate has very different requirements from a retail palette that will ride in handbags, survive bathroom humidity, meet sunscreen oils and be reviewed on social media. The material choice is a commercial decision as much as a technical one, and the rest of this guide gives you the framework to make it deliberately rather than by default.
Five polymers dominate cosmetic compact and palette construction. Understanding where each fits prevents the most common specification mistake: asking one material to do the job of another.
| Material | Typical palette role | Transparency | Impact behavior | Decoration suitability | Relative cost |
|---|---|---|---|---|---|
| ABS | Structural shell, caps, closures, electroplated frames | Opaque | Very rigid, high impact strength | Excellent — plating, painting, hot stamping, texture | Low to medium |
| PETG | Clear lids, windows, trays, premium one-piece cases | Very high, glass-like | Tough, slightly flexible | Good — tinting, printing with special inks | Medium |
| PMMA (acrylic) | Luxury clear lids, jewel-like lids, high-clarity windows | Highest optical clarity | Brittle, scratches visibly | Excellent polish, laser engraving | Medium to high |
| PP | Inner trays, pan holders, low-cost shells, living hinges | Natural translucent | Flexible, fatigue-resistant hinges | Limited — needs surface treatment for ink | Lowest |
| PC (polycarbonate) | High-impact clear components (declining due to BPA concerns) | High | Extremely tough | Good, but market acceptance falling | Medium to high |
Three practical observations follow from this table. First, PMMA looks the most luxurious on a shelf but is the most fragile in a handbag — it is a deliberate trade-off, not an upgrade. Second, PP earns its place not through looks but through hinge fatigue life; a PP-based inner mechanism can survive tens of thousands of open-close cycles. Third, ABS and PETG are not competitors for the same part so much as partners in the same assembly: ABS carries the load and the decoration, PETG carries the light.

PETG is glycol-modified polyethylene terephthalate. The glycol modification changes the crystallization behavior of ordinary PET, producing an amorphous, crystal-clear material that injection molds without the haze that plague unmodified PET in thick sections. For palette buyers, four properties matter.
Clarity and perceived value. PETG transmits roughly 90 percent of visible light with very low haze, which lets a filled palette show its shades through a closed lid — a genuine merchandising advantage for open-sell retail and e-commerce listings where the consumer photographs the product. Thick-walled PETG also mimics the visual weight of glass at a fraction of the cost, which is why premium powder compacts and serum-adjacent packaging use it so heavily.
Chemical resistance. PETG resists the alcohols, glycols and diluted acids common in cosmetic vehicles better than many other clear plastics. Pressed powders, cream shadows and gel liners stored in direct contact with PETG wells generally show no crazing. The known weak spots are certain essential oils and strong solvents, which can haze the surface — if your formula is oil-rich, request a compatibility coupon test before committing.
Toughness. PETG does not shatter the way PMMA does. A dropped PETG lid usually survives; it may scuff. That scuffing is the material's main cosmetic weakness — PETG surfaces scratch more readily than coated ABS or hard acrylic, so surface protection films during assembly and transit packaging matter.
Processing behavior. PETG processes at lower temperatures than ABS (roughly 200–230 °C barrel temperatures versus 220–260 °C), which shortens cycle times slightly and reduces energy cost. It is, however, hygroscopic: resin must be dried thoroughly before molding, or the parts show silver streaks and reduced clarity. Ask a prospective supplier how they dry and store PETG resin — the answer is a surprisingly reliable indicator of overall process discipline.
ABS — acrylonitrile butadiene styrene — is a three-monomer terpolymer engineered for rigidity, dimensional stability and surface quality. In palette construction it plays the role that a frame plays in a building: everything else hangs off it.
Rigidity and the closure experience. The "satisfying click" of a well-made compact is an ABS property. The material's high flexural modulus keeps closure tabs within tolerance over thousands of open-close cycles, so snap force stays consistent from the first use to the last. PETG, being more flexible, tends to produce a softer, mushier closure feel in snap-fit designs — one reason hybrid designs put the snap features in ABS.
Decoration versatility. ABS is the single most decoration-friendly plastic in the beauty industry. It accepts vacuum metallization (chrome and gold effects), spray painting, soft-touch rubber coatings, UV coatings, hot stamping foil and silk-screen inks with excellent adhesion. If the brand direction calls for a metallic frame, a piano-black lid or a matte-touch shell, ABS is usually the correct base. The same decoration stack on PETG or PP requires primers or special ink systems and often looks less uniform.
Precision for assemblies. Palettes are assemblies: mirror recesses, pan seats, magnet pockets, hinge pins. ABS holds tight tolerances (±0.05 mm is routine on SMALL features) and its opacity hides the adhesive and structural ribs inside the shell. This makes it the natural material for the base and any part that must locate another part.
Limitations. ABS is opaque, so it cannot deliver see-through merchandising on its own. Its chemical resistance to some fragrance and oil systems is weaker than PETG's — prolonged contact with certain citrus oils can craze painted ABS surfaces. And it is a petroleum-derived styrenic, which matters for brands with sustainability narratives; recycled ABS and bio-based ABS exist but with limited color consistency and supply.

The table below condenses the decision into the properties that actually change outcomes in production and in use. It assumes a twelve-pan rectangular palette with a mirror and magnetic closure — the most common format — but the logic scales to singles and quads.
| Property | ABS | PETG |
|---|---|---|
| Clarity | Opaque (natural; colored by pigment) | Water-clear, about 90 percent light transmission |
| Flexural rigidity | High — crisp closure, stable geometry | Moderate — flexible walls at thin gauge |
| Impact at low temperature | Good, can embrittle below minus 20 °C | Excellent, stays tough |
| Chemical resistance | Moderate; some oils craze coatings | High for alcohols and glycols; weak to some essential oils |
| Decoration | Plating, painting, stamping — all first-class | Tinting and clear printing; coating systems limited |
| Scratch visibility | Concealable with texture and coating | Visible on clear surfaces; needs film protection |
| Mold temperature window | 220–260 °C, wide process window | 200–230 °C, requires dry resin |
| Recyclability story | Widely recycled styrenic stream | Polyester stream, theoretically recyclable |
| Best palette role | Shell, base, closures, plated frames | Lid window, tray, full-clear lid, travel tins |
Two hybrid patterns dominate well-engineered palettes. The first is the ABS shell plus PETG window: the brand keeps structural confidence and decoration freedom while still showing the shades. The second is the PETG body plus ABS mechanism: fully Transparent travel palettes use a PETG case with small ABS snap bosses and hinge elements where fatigue matters. In both cases the adhesive and welding choice (UV-cure adhesive for mirror seating, ultrasonic welding for shell joints) must be validated on the specific resin pair, because adhesive bonds that hold ABS beautifully can fail on PETG's lower surface energy.
Cosmetic packaging is regulated indirectly: the palette itself is not a cosmetic, but it contacts a product applied to skin, so supply chains verify material safety through a framework of standards and declarations. The table below lists the documents a professional buyer should request, per market.
| Market | Framework / Standard | What it covers | What to ask the supplier for |
|---|---|---|---|
| United States | FDA 21 CFR relevant sections; CPSIA for giveaways | Substances acceptable for indirect skin-contact logic; children's product safety for novelty items | Declaration of composition and CFR citations for resins and coatings |
| European Union | REACH (EC 1907/2006) including SVHC screening; EU Packaging Directive | Substance restrictions, SVHC content above thresholds, packaging recyclability labeling | REACH SVHC test report from an accredited lab, dated within 12 months |
| Global | ISO 22716 cosmetics GMP | Factory hygiene, traceability and process control for cosmetic-contact packaging | Valid ISO 22716 or ISO 9001 certificate with scope covering injection molding |
| Marketplaces | RoHS-style heavy metal screening (Pb, Cd, Hg, Cr6+) | Heavy metals in coatings, inks and plating | Heavy metal scan on the decorated part, not just the raw resin |
| Transport | ISTA 1A / 2A or equivalent transit test | Drop, vibration and compression survival of the packed product | Transit test report for the actual retail packaging, not a generic box |
A recurring trap is testing raw resin instead of the finished decorated part. Plating baths, paints and inks introduce their own chemistry, and a heavy-metal or SVHC failure on the coating — not the resin — is what gets a shipment blocked. Insist that the certificate numbers refer to the final assembled, decorated article in the colorway you are ordering, and re-test on an annual cycle or whenever a supplier changes a coating vendor.
Returns and negative reviews cluster around a small number of failure modes. Knowing them tells you exactly which questions to ask and which bench tests to demand.
Hinge cracking. A flip-top hinge in ABS that was molded with a cold gate or excessive packing stress will show white stress marks and then crack after a few hundred cycles. The fix is process control, not material change: gate location away from the hinge, proper mold temperature, and hinge-cycle validation (20,000 cycles minimum for retail palettes). If a supplier cannot show a hinge cycling video or report, treat the quote as unproven.
Stress cracking from formulas. Cream and liquid products containing oils or high alcohol can crack ABS wells under residual molded-in stress — the classic pattern is a radial crack around a pan seat appearing weeks after filling. PETG resists this better, and stress-relief annealing of ABS pans helps. If your formula is oil-based, request a 30-day loaded compatibility test at 40 °C.
Mirror delamination. Mirrors are glass with a silvered or aluminum backing and a protective paint layer. In humid climates, edge ingress lifts the backing and produces black spots. Buyers should specify edge-sealed mirror stock and require a damp-heat test (for example, 48 hours at 40 °C and 90 percent relative humidity) on assembled units.
Plating and paint peel. Vacuum-metallized ABS frames peel when the base coat cure was incomplete or when the part was touched with bare hands before plating. Cross-hatch adhesion testing (ISO 2409, target class 0–1) on every production batch catches this before shipment.
Magnet pull-out and closure drift. Neodymium magnets glued into shallow pockets migrate or drop out if the adhesive is under-specified. Verify magnet retention by pull-force measurement on sampled units and confirm the pocket design uses both adhesive and a mechanical undercut where possible.
Pan retention failures. Empty pans are either glued or heat-staked into trays. Glued pans lift out in transit; heat-staked PETG trays hold better but require tooling investment. Ask how pans are retained and test with a full-pan loading at the maximum your program will use.
Verification is a ladder of evidence, each rung cheaper than discovering the same defect in a container of finished goods.
Document review. Start with resin data sheets naming the actual grade (not "PETG, food grade"), the certificate package from the table above, and mold drawings showing gate locations and ejection layout. A factory that sends a real datasheet with grade numbers and a dated test report is categorically different from one that sends a glossy brochure.
Golden samples and color standards. Approve a signed golden sample set — one for the molder, one for you, one sealed for dispute resolution — plus Pantone-matched color plaques for every colored component. All subsequent production is judged against these, not against memory or photographs.
Bench tests you can run yourself. Simple tests reveal a lot: drop a packed sample from 1.0 m onto concrete on each face; cycle the hinge 200 times by hand and check for whitening; wipe a decorated surface with a 50 percent ethanol wipe ten times and inspect for dulling; weigh magnetic closure force with a pull gauge (a typical target is 4–8 newtons for travel palettes). These tests cost nothing and correlate well with field performance.
In-process checkpoints. For bulk production, define three hold points: first-off approval at machine start, in-line dimension checks on pan seats and closure tabs every two hours, and end-of-line AQL inspection (typically ANSI/ASQ Z1.4 level II, AQL 1.5 for major defects). Put these in the purchase contract, not in an email thread.

Pan compatibility is where design intent and manufacturing reality collide. The industry's most common round pan diameters are 26 mm and 36 mm, with larger formats for singles; rectangular palettes use standardized pan strips or custom wells. The table below summarizes typical reference dimensions buyers use in RFQs.
| Format | Common pan size | Typical depth | Retention method | Design notes |
|---|---|---|---|---|
| Single compact | Diameter 36 mm | 3–5 mm | Adhesive or snap ring | Allow 0.2 mm diametral clearance plus adhesive budget |
| Quad palette | Diameter 26 mm, four wells | 3–4 mm | Heat-staked tray | Check gantry spacing for filling-line pick tools |
| 8–12 pan palette | Diameter 26 mm grid | 3–4 mm | Heat-staked or glued | Mirror often sits under the lid — verify lid drop depth |
| Rectangular pro palette | Pan strips 26 by 76 mm | 4–8 mm | Magnetic tray base | Specify magnet count per strip for equal pull |
Ask each candidate factory for its standard tooling in these formats before requesting custom tooling quotes. Standard formats ship faster, cost less and carry proven pan-interference data; custom formats make sense only when the palette silhouette itself is the brand asset. When custom tooling is justified, budget for a first-sample iteration and expect 30–45 days from mold design to first samples, with a further 5–10 days for corrections.
Minimum order quantities in palette packaging follow a simple hierarchy. Stock-mold palettes (existing tools, standard colors) often start at 1,000–3,000 units, because the factory only carries material and decoration cost. Custom colors on stock tools typically require 3,000–5,000 units to justify a dedicated color run. Fully custom tooling usually begins at 5,000–10,000 units and requires tooling investment amortized either upfront or across orders.
Tooling economics deserve a moment of buyer attention. A single-cavity palette shell mold and a lid mold together can represent a significant capital line; multi-cavity tools reduce per-unit cost but raise the entry price. Ask for the mold ownership terms in writing — who owns the steel, what happens if production stops, and what the maintenance obligations are. These terms matter more than a small unit-price difference over a multi-year program.
Packaging is not an afterthought for palettes, because mirrors and clear lids are transit-fragile. Standard export practice is an individual polybag or foam sleeve, then a divider carton, then a master carton with drop-test evidence. If retail-ready boxes are in scope, define flute type, inner fit and a pallet pattern. Verify the packed dimensions against your freight plan: air freight on volumetric weight can double the logistics cost of a lightweight palette program, which is one more reason wall thickness and assembly size belong in the earliest cost conversations.
Finally, request a costed bill of materials from each shortlisted supplier: resin, pans, mirror, magnets, adhesive, decoration, assembly labor and packaging, each priced separately. Comparing BOMs exposes where one quote includes a heat-staking operation another omitted, and prevents the classic "lowest quote, then surprise surcharges" pattern.
Q1: Is PETG safer than ABS for cosmetic packaging?
Both materials are widely used and can be compliant when produced from virgin resin with proper documentation. "Safer" is determined by the certificate package — REACH SVHC screening, heavy-metal scans on decorated parts and factory GMP — not by the polymer name. Request the paperwork and the material question resolves itself.
Q2: Can a palette use both ABS and PETG in one assembly?
Yes, and most professional designs do: ABS for the structural shell and closure features, PETG for the window or clear lid. Validate the adhesive or mechanical joint between the two, since bond strength differs across resin pairs.
Q3: What closure force should a magnetic palette have?
For travel sizes, 4–8 newtons of pull is a common working range — enough to survive a handbag, light enough for one-hand opening. Test on finished units with a pull gauge rather than trusting magnet grades alone, because pocket depth and steel inserts change the effective force.
Q4: How many open-close cycles should a palette hinge survive?
Retail quality benchmarks usually demand 20,000 hinge cycles without cracking or loss of more than 20 percent closure force. Promotional-grade products may accept less, but the number should be agreed in writing either way.
Q5: Why did my clear palette lid turn hazy after weeks on the shelf?
Haze on PETG usually traces to one of three causes: resin dried inadequately before molding, exposure to solvent-rich cleaning agents, or contact with certain essential oils. Confirm the molding house's resin-drying practice and run a formula-contact coupon test before the next order.
Q6: What is a realistic first-article timeline for a custom palette?
Plan on 30–45 days for mold design and build, 5–15 days for the first sample round, and 1–2 correction iterations before production release. Quoted timelines significantly shorter than this usually mean stock tools — which is fine, as long as the design was chosen with that constraint in mind.
The PETG-versus-ABS question resolves into a parts question. ABS delivers rigidity, precision and first-class decoration, which makes it the right shell for palettes whose value lives in structure and finish. PETG delivers glass-like clarity with genuine toughness, which makes it the right lid, window and tray wherever showing the product is the point. The strongest palette programs stop treating this as a rivalry and start specifying the assembly: ABS where loads and closures live, PETG where light and merchandising live, and a validated joint between them.
Verification is what separates a professional order from a gamble. Ask for named resin grades rather than marketing labels, dated certificates covering the decorated finished article, hinge-cycle and drop evidence on real assemblies, and a costed BOM that exposes exactly what each quote includes. Run the zero-cost bench tests — drops, cycles, wipes, pull forces — on golden samples and again at first production. None of this requires a laboratory; it requires a checklist and the discipline to use it.
Approached this way, material selection becomes a controllable engineering decision instead of a supplier-driven default. Buyers who document the resin, the tests and the tolerances get palettes that survive the handbag, the transit carton and the social-media close-up — and a supply relationship built on evidence ages far better than one built on photographs.
Jinhua Xingqiao Plastik Industry Co, Ltd.
 Ponsel: +008613868982062
 Telepon: +86-579-82196667
 Faks: +86-579-82196656
 E-mail:penjualan@zjxqpackaging.com
 Situs web:http://www.zjxqpackaging.com
 Alamat: tidak. 377, Jalan Yongxue, distrik kota w U, kota jin, provinsi Z Hejiang
Hak Cipta © 2022 Jinhua Xingqiao Plastic Industry Co., Ltd
Situs web ini menggunakan cookie untuk memastikan Anda mendapatkan pengalaman terbaik di situs web kami.
 English



 Telepon
Komentar
(0)